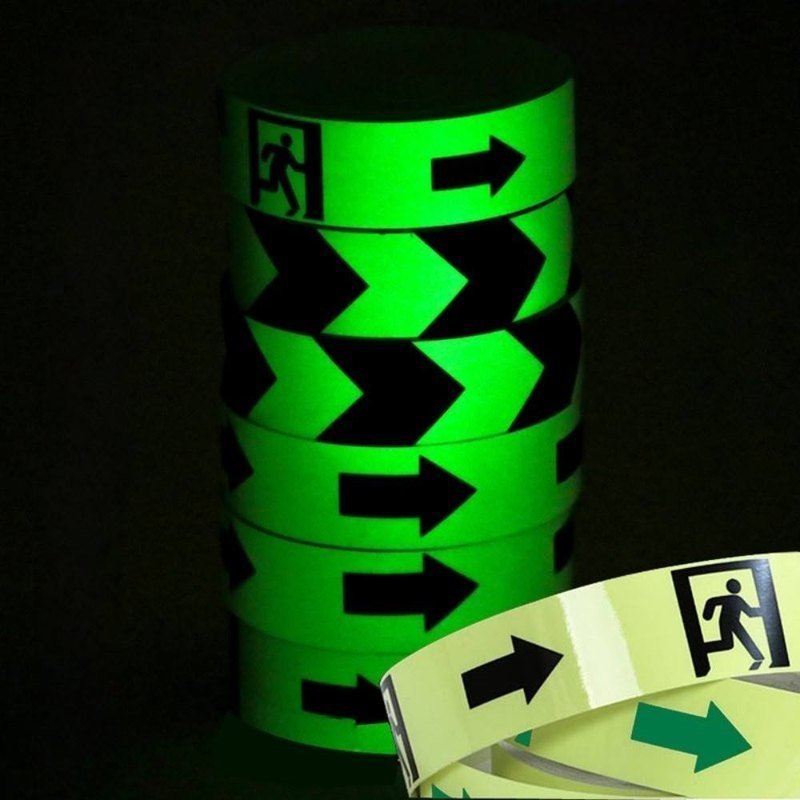
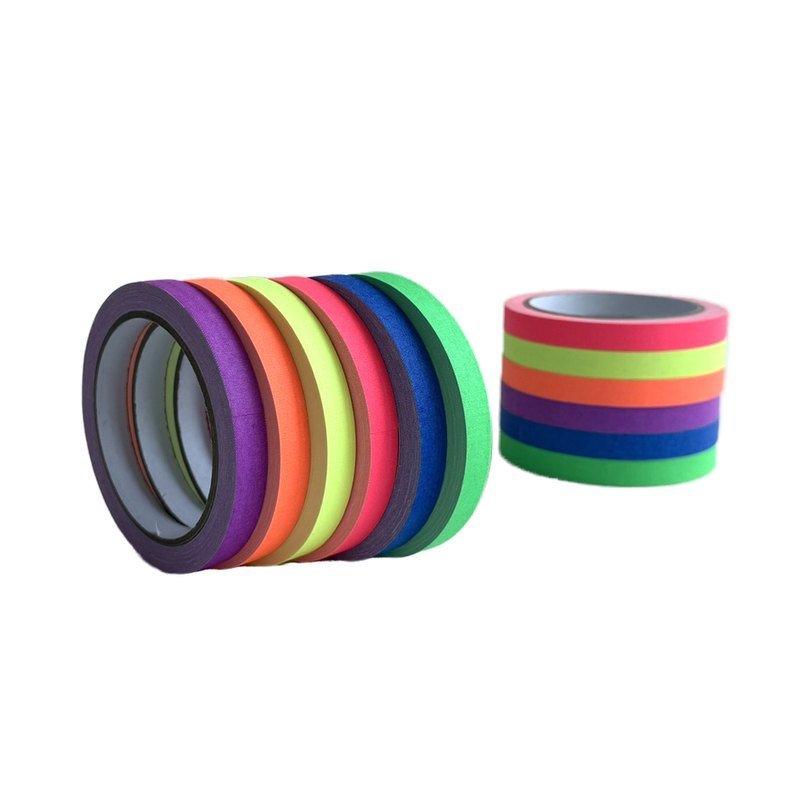
A roll is the cheapest way to mark a straight line, but it cannot produce an arrow, a pictogram or a shape that follows a moulded panel. Die cutting converts the same tape into parts that an installer can place without measuring. The economics change when labour on site costs more than the tooling, which is common in fit-out and OEM work.
Tooling and tolerances
A steel rule die is the usual tool for tape parts, and its cost depends on the perimeter and complexity of the shape. Tolerances of about plus or minus 0.5 mm are realistic for a kiss-cut part on a liner; tighter tolerances raise tool cost and slow production. Very fine details, such as thin arrow tails, tend to lift and should be avoided in a pressure-sensitive material.
- Kiss cut: part stays on a liner sheet for easy handling
- Through cut: individual parts supplied loose in a bag
- Perforated sheet: parts stay together until torn off on site
- Roll format: high volume, applied by a dispensing machine
Artwork and packing
Supply vector artwork at final size with the cut line on a separate layer. Confirm the orientation on the liner, because a part that peels in the wrong direction slows installation. Packing should protect the liner from curling: flat sheets in a carton with a card between layers work better than a tight roll, especially for larger shapes.
What to send for a quote
Provide the shape drawing, overall size, quantity per shape, liner preference and the substrate the part will be applied to. State whether the part needs anti slip grit as well as luminance, since that changes the material and the cutting behaviour. A supplier can then quote tooling, unit price and lead time without a round of clarification that delays the project.